Environmental protection equipment supplier
How does the integrated spoiler-spray deodorization system achieve efficient odor removal?
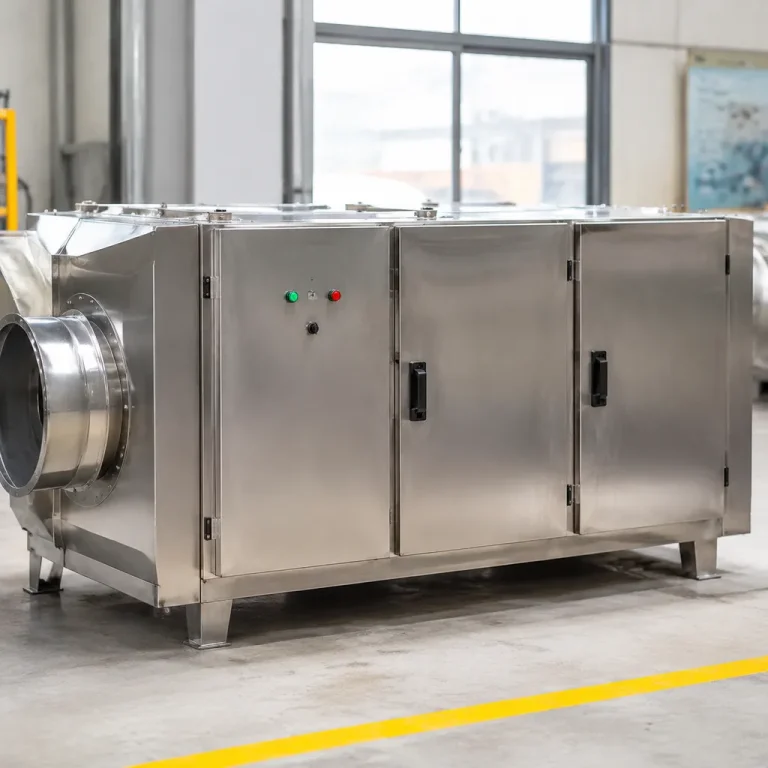
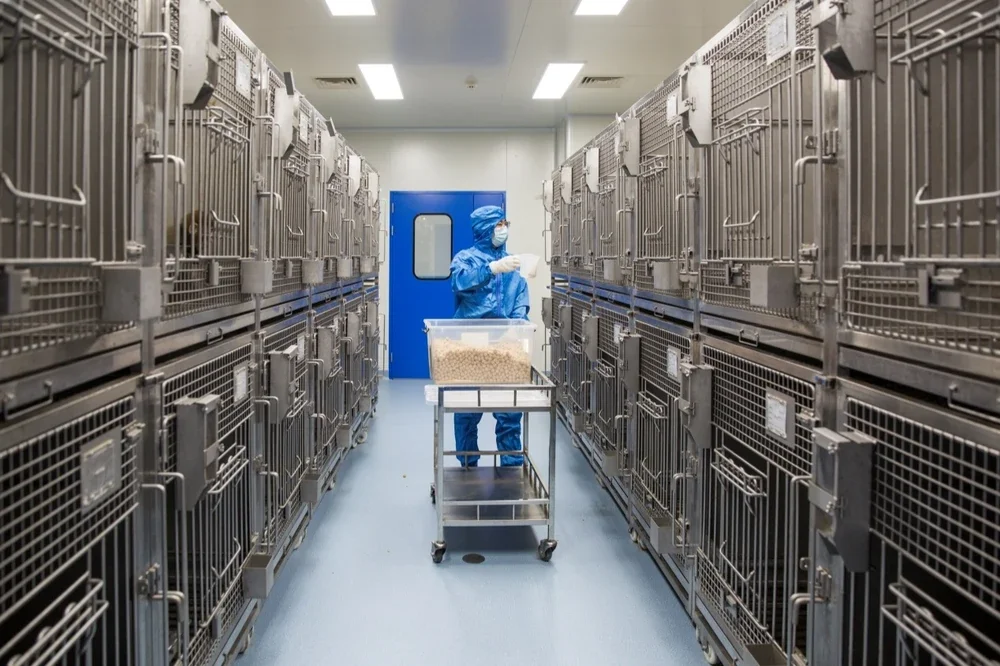
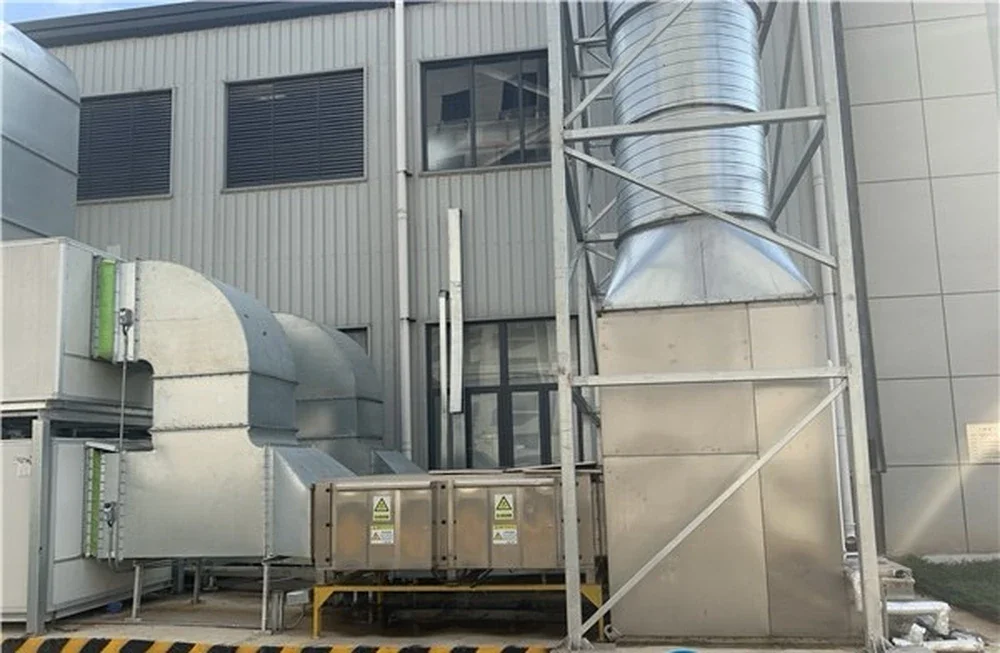
Combining physical and chemical processes, the integrated turbulent-flow spray deodorization system delivers 24/7 odor and waste-gas purification—98% purification rate and ≥99% desulfurization—for laboratory animal facilities, pharmaceutical plants, and livestock farms.Additionally, the system features low airflow resistance and controllable energy consumption, making it suitable for treating high-concentration waste gases.
Technical Principles and Core Structure:
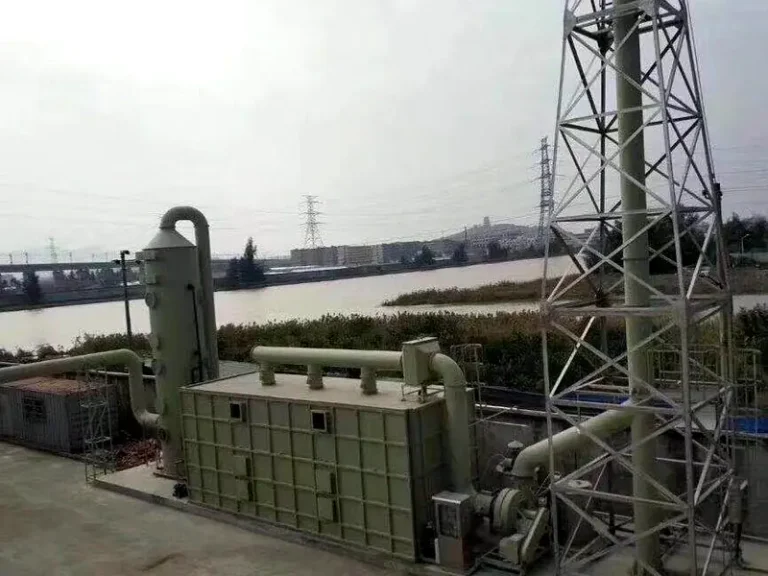
This equipment utilizes “turbulent spray plus multi-stage purification” technology. High-pressure nozzles atomize a specialized absorption solution into micron-sized droplets, ensuring thorough contact and neutralization reactions with odorous molecules—such as hydrogen sulfide and ammonia—present in the waste gas. Internal flow-disrupting baffles extend gas residence time to guarantee complete reaction, while an intelligent DDC control system dynamically balances operations by automatically adjusting spray volume and airflow velocity based on real-time waste gas concentration monitoring.With its 304 stainless steel construction and 300 MPa compressive strength, the unit withstands demanding industrial environments.
Performance Parameters and Application Scenarios:
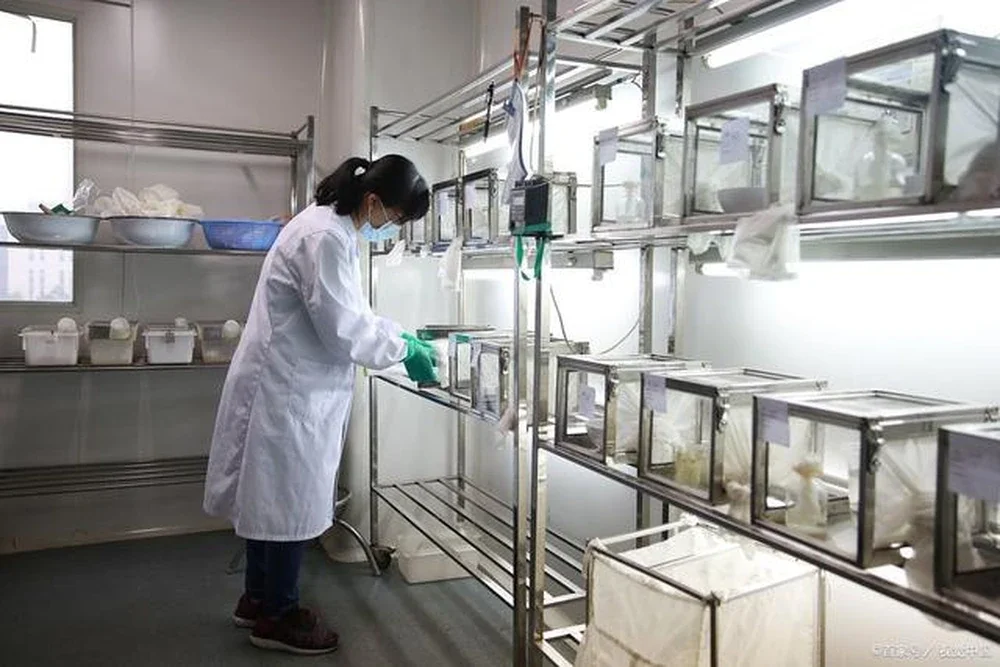
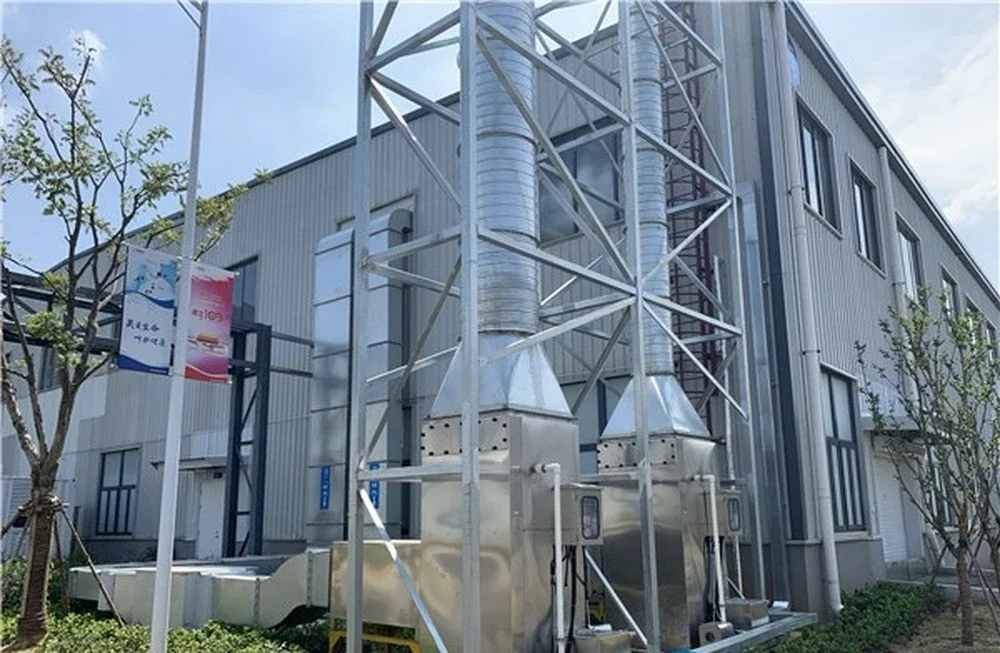
II. The equipment features a rated air treatment capacity of 50,000 m³/h and an air velocity of 2.3 m/s; it is capable of handling high-concentration waste gas (up to 200 mg/L) with a low light-off temperature of just 200°C, resulting in reduced energy consumption. Emissions comply with the GB14554-93 standard, making the system suitable for environments requiring “5-star” purification levels, such as laboratory animal facilities, pharmaceutical plants, and livestock farms. For instance, in livestock farms, the equipment effectively decomposes ammonia generated from animal waste, thereby lowering the risk of respiratory diseases; in pharmaceutical plants, it treats VOCs emitted from organic solvents, preventing cross-contamination.
Operation Method and Safety Design:
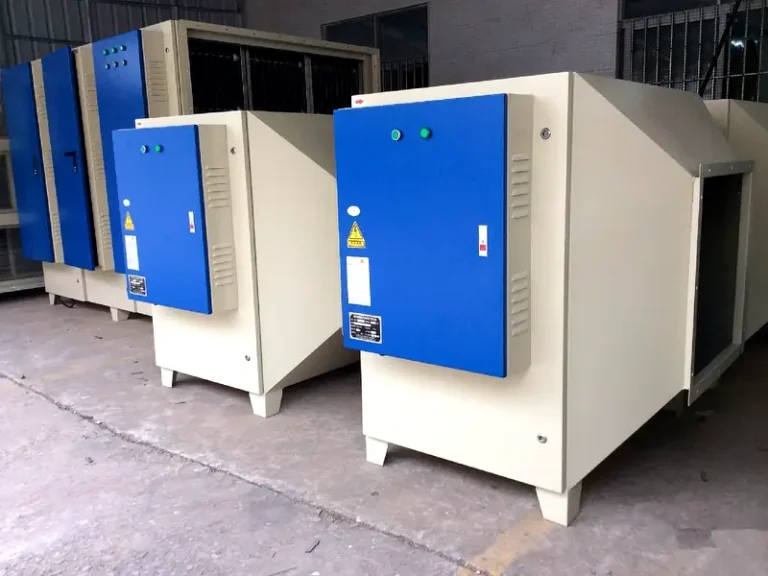
The equipment features a modular design and requires a 380V (50Hz) power supply rated at 4600W. Operators can configure parameters such as start/stop times and spray frequency via the DDC control panel. Routine maintenance only involves periodically replenishing the absorption liquid and clearing nozzle blockages. With an airflow resistance of only 350 Pa, the unit has minimal impact on the existing ventilation system.For safety, the equipment incorporates built-in temperature sensors and pressure monitoring devices. It automatically triggers an alarm and shuts down upon detecting abnormal ignition temperatures or excessive airflow resistance, thereby preventing potential safety hazards.
Technical Highlights and Real-World Performance:
Compared to traditional spray towers, this equipment boosts purification efficiency by 30% through a flow-disruption design while reducing energy consumption by 20%. Its integrated structure minimizes piping connections, thereby lowering the risk of leaks; constructed from 304 stainless steel, it offers excellent corrosion resistance and a service life exceeding 10 years.